Oct 13, 2026Ultrasonic Cleaning Technology
How to Tell If an Ultrasonic Cleaner Is Working Properly: Cavitation Checks and Troubleshooting
Learn how to tell if an ultrasonic cleaner is working properly by checking liquid level, degassing, cleaning action, foil test results, uneven cavitation, loading, bath condition, and process variable
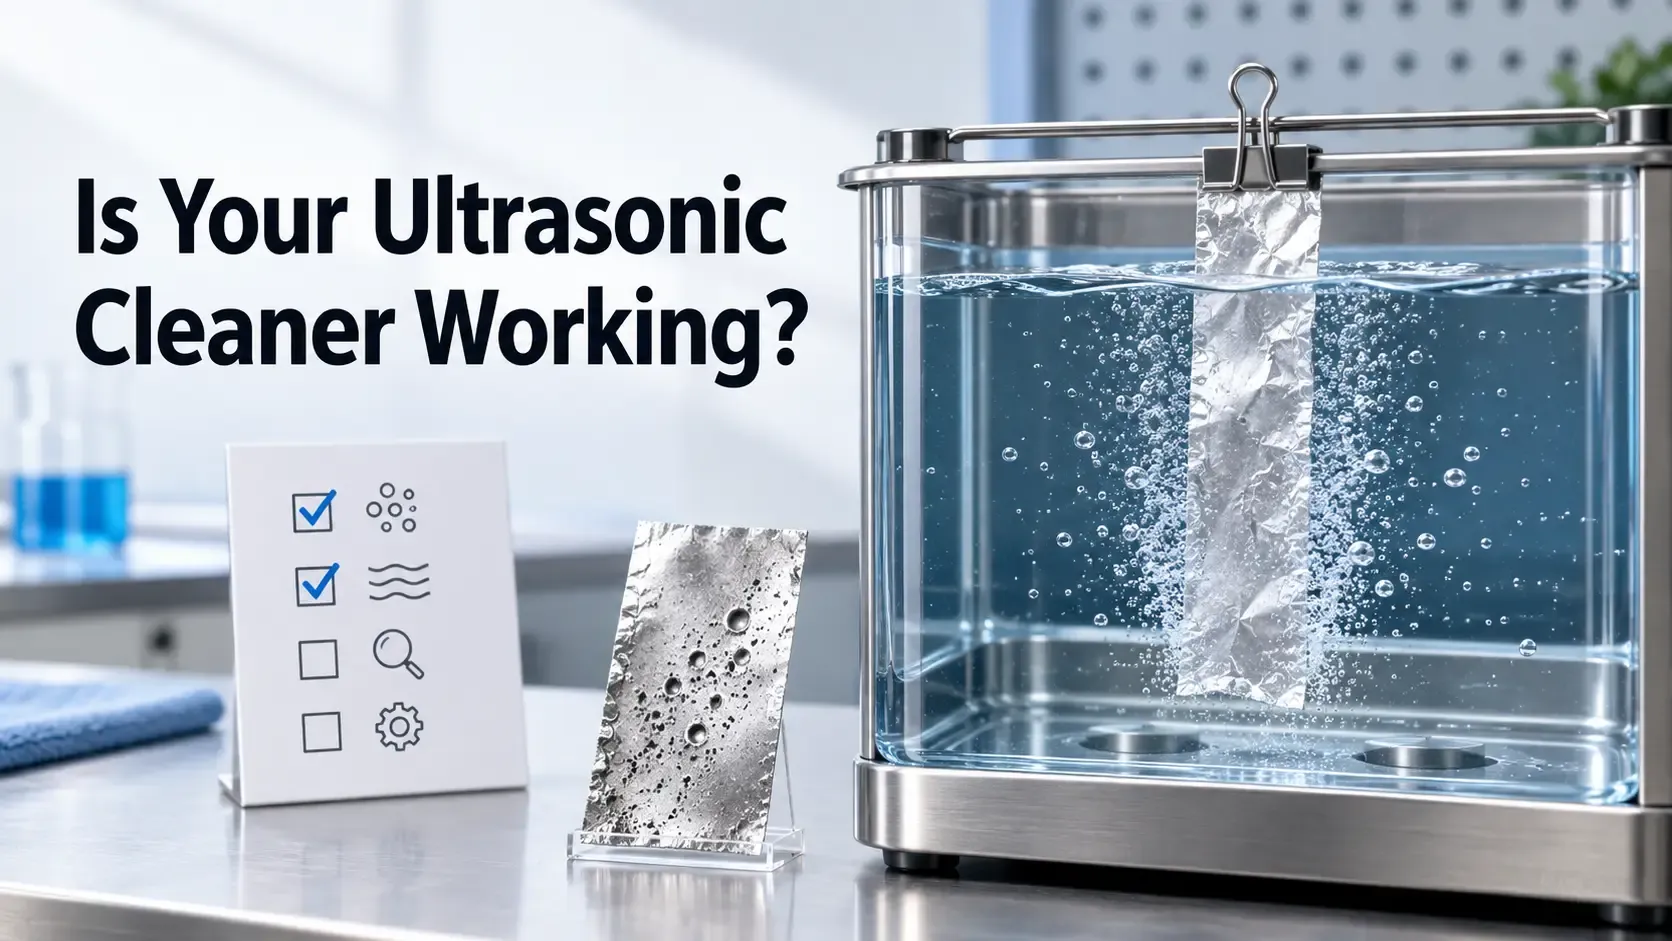
An ultrasonic cleaner can make sound, heat the liquid, and run through a timer cycle, but that does not always prove it is cleaning properly.
For many users, the confusing question is:
Is the ultrasonic cleaner actually working, or is the cleaning process wrong?
Poor cleaning results may come from the machine itself, but they are frequently caused by incorrect liquid level, improper cleaning solution, missing degassing, poor loading, an exhausted bath, unsuitable temperature, or parts that are difficult to clean.
This guide explains how to check whether an ultrasonic cleaner is working properly without turning it into an electrical repair manual.
Quick Answer
To tell if an ultrasonic cleaner is working properly, start with simple process checks before assuming the machine has failed.
Check these core areas:
- correct liquid level in the tank
- suitable cleaning solution and correct concentration
- proper liquid degassing
- stable bath temperature
- appropriate basket choice and part loading
- visible cleaning action on known test parts
- even cavitation distribution across the tank
- foil test results as a practical cavitation reference
- whether cleaning performance has changed compared with earlier operation
A foil test can help show whether cavitation is present and whether activity is uneven, but it is not a complete performance certification. If the machine shows weak or uneven cavitation after basic process checks, contact your supplier instead of opening electrical components yourself.
Sound Alone Does Not Prove the Cleaner Is Working
Many ultrasonic cleaners produce a buzzing or humming sound during operation.
That sound may indicate that the machine is running, but it does not prove that cavitation is strong, even, or suitable for the cleaning task.
An ultrasonic cleaner can make noise while still cleaning poorly if:
- the liquid level is incorrect
- the solution has not been degassed
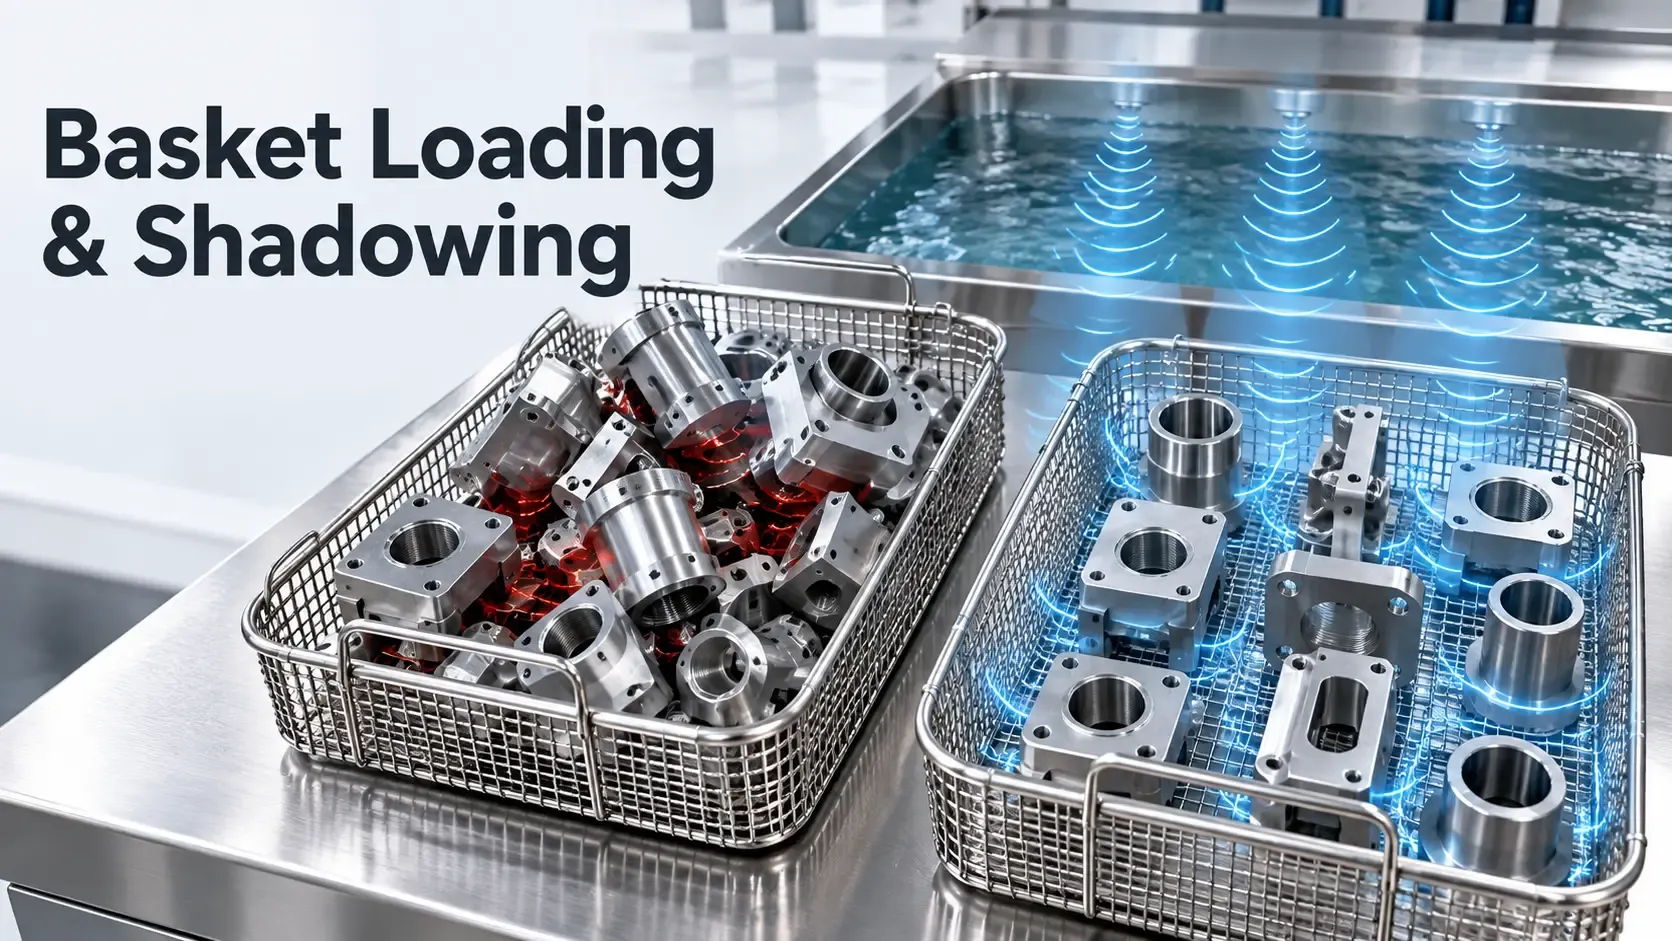
- the bath is overloaded with parts
- the basket blocks ultrasonic energy
- the cleaning solution is wrong
- cavitation is uneven across the tank
- the parts have complex geometry or stubborn contamination
- equipment performance has changed over time
Do not judge ultrasonic performance by sound alone.
A better approach is to check the setup, observe cleaning behavior, and use simple cavitation reference tests.
1. Check the Basic Setup First
Before testing the machine, confirm that the operating setup is correct.
Basic setup problems can make a healthy machine appear weak.
Check:
- Is the tank filled to the recommended working liquid level?
- Is the cleaning solution suitable for the specific contamination?
- Is the detergent concentration mixed correctly?
- Has the bath been degassed?
- Is the temperature appropriate for the chemistry and part material?
- Is the basket or fixture blocking ultrasonic action?
- Are too many parts loaded at once?
- Are parts resting directly against the tank bottom?
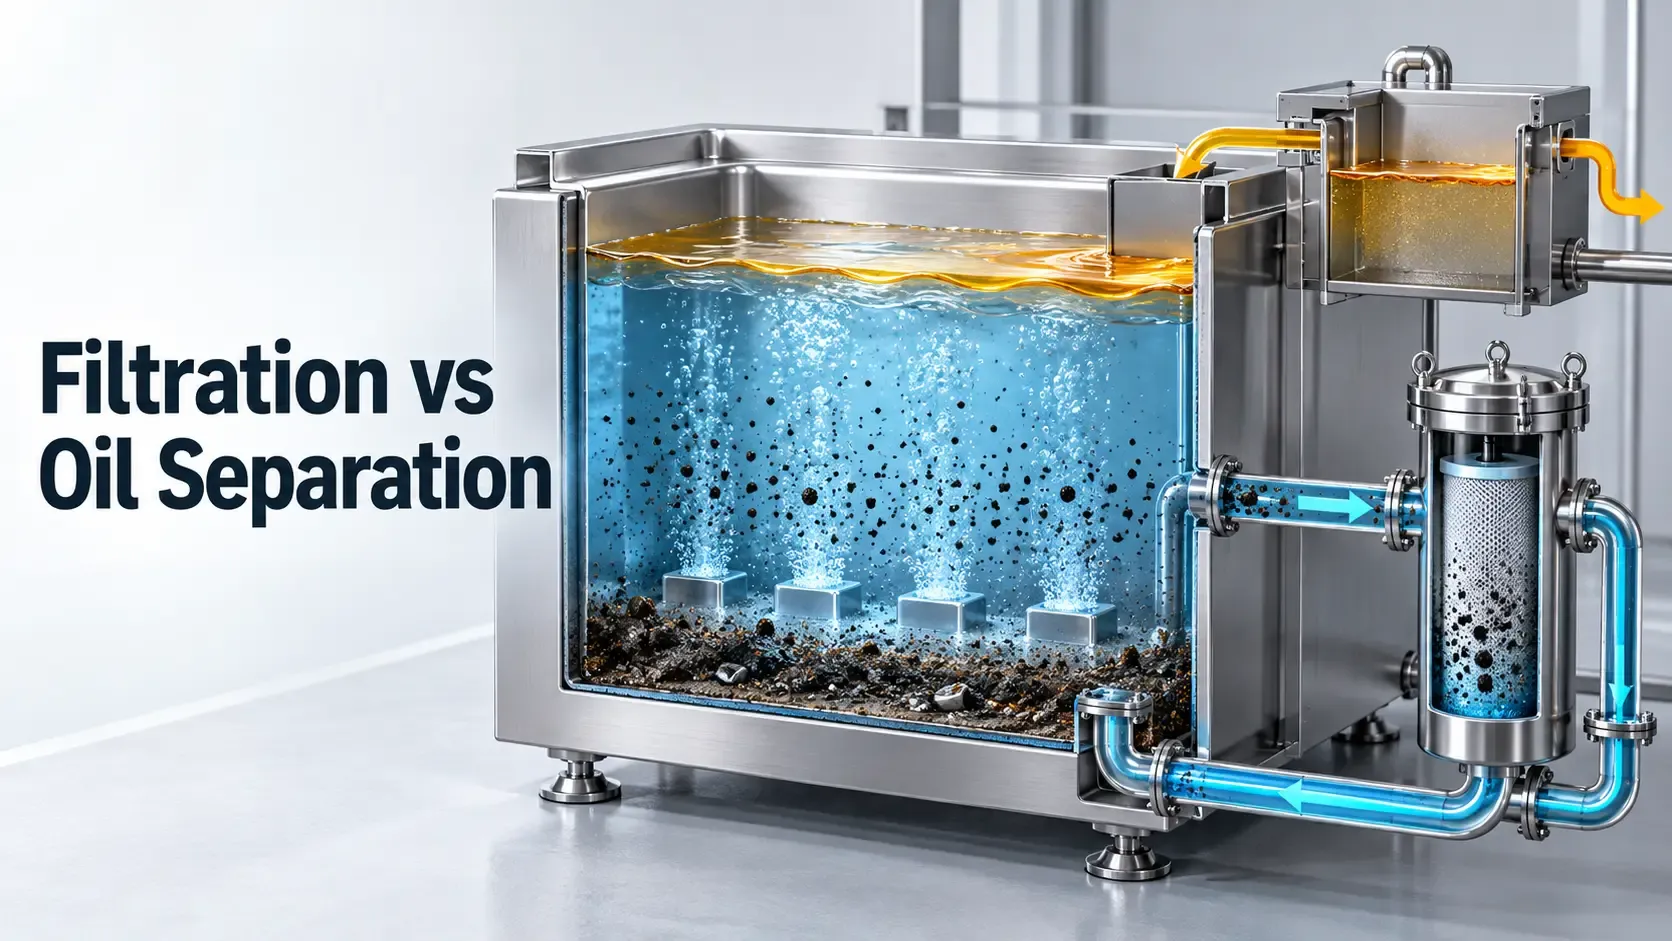
- Is the bath dirty, oily, or exhausted?
If these conditions are wrong, the machine may not clean properly even if the ultrasonic system is functioning.
2. Degassing Can Affect the First Cleaning Cycles
Fresh water or newly mixed cleaning solution can contain dissolved air.
This trapped air can absorb ultrasonic energy and reduce effective cavitation, especially during the first cycles after refilling the tank.
If the machine seems weak right after a bath change, degassing may be needed.
Some machines feature a dedicated degas mode. Others can be run without parts for a short period before cleaning to help drive trapped air out of the solution.
The required time depends on tank size, liquid volume, solution type, temperature, and machine design.
Degassing will not fix every cleaning issue, but it is a basic check before assuming the machine is faulty.
3. Look for Cleaning Action, Not Just Bubbles
Visible bubbles do not automatically mean effective ultrasonic cavitation.
Some bubbles may result from trapped air, heating, detergent foaming, or mechanical agitation.
Instead of judging by bubbles alone, look for cleaning results:
- Does a lightly contaminated test piece become visibly cleaner within the cycle time?
- Are similar parts cleaned consistently across separate batches?
- Does cleaning performance improve after degassing?
- Does performance improve when the basket load is reduced?
- Are certain areas of the tank cleaning weaker than others?
- Has cleaning efficiency declined compared with earlier use?
A machine may show activity in the liquid but still fail to clean if the process is wrong or the part geometry is difficult.
4. Use a Foil Test as a Simple Cavitation Reference
A foil test is a practical, low-cost method to check cavitation activity and distribution across an ultrasonic tank.
A simple foil test process is:
- Fill the tank to its normal working level with water or the recommended test liquid.
- Degas the bath if needed.
- Suspend a sheet of standard aluminum foil vertically in the tank using clips or a simple holder.
- Run the ultrasonic machine for a short test cycle.
- Remove the foil and inspect it for pitting, frosting, small perforations, or erosion marks.
Typical observations:
- active cavitation: the foil shows visible pitting, frosting, or small holes
- weak or absent cavitation: the foil remains largely smooth or unmarked
- uneven cavitation: marks appear only in localized areas
The foil should not rest flat on the tank bottom or directly touch the side walls during the test.
5. What a Foil Test Can and Cannot Tell You
A foil test is useful, but it has clear limits.
It can help show:
- whether cavitation is active in the tank
- whether cavitation distribution is uneven or localized
- whether machine performance appears weaker than past reference tests
- whether setup adjustments affect cavitation activity
It cannot prove:
- that every specific part geometry will clean successfully
- that the machine meets formal engineering performance standards
- that the cleaning chemistry or temperature is correct
- that the machine is free from underlying wear
- that a difficult production process is validated
Foil test results can vary depending on:
- foil thickness
- liquid level
- water or solution type
- degassing condition
- temperature
- tank size
- test position
- test duration
Use the foil test as a practical reference tool, not as a final laboratory certification.
For critical cleaning processes, follow equipment supplier guidance and any internal validation requirements.
6. Check for Uneven Cavitation or Dead Zones
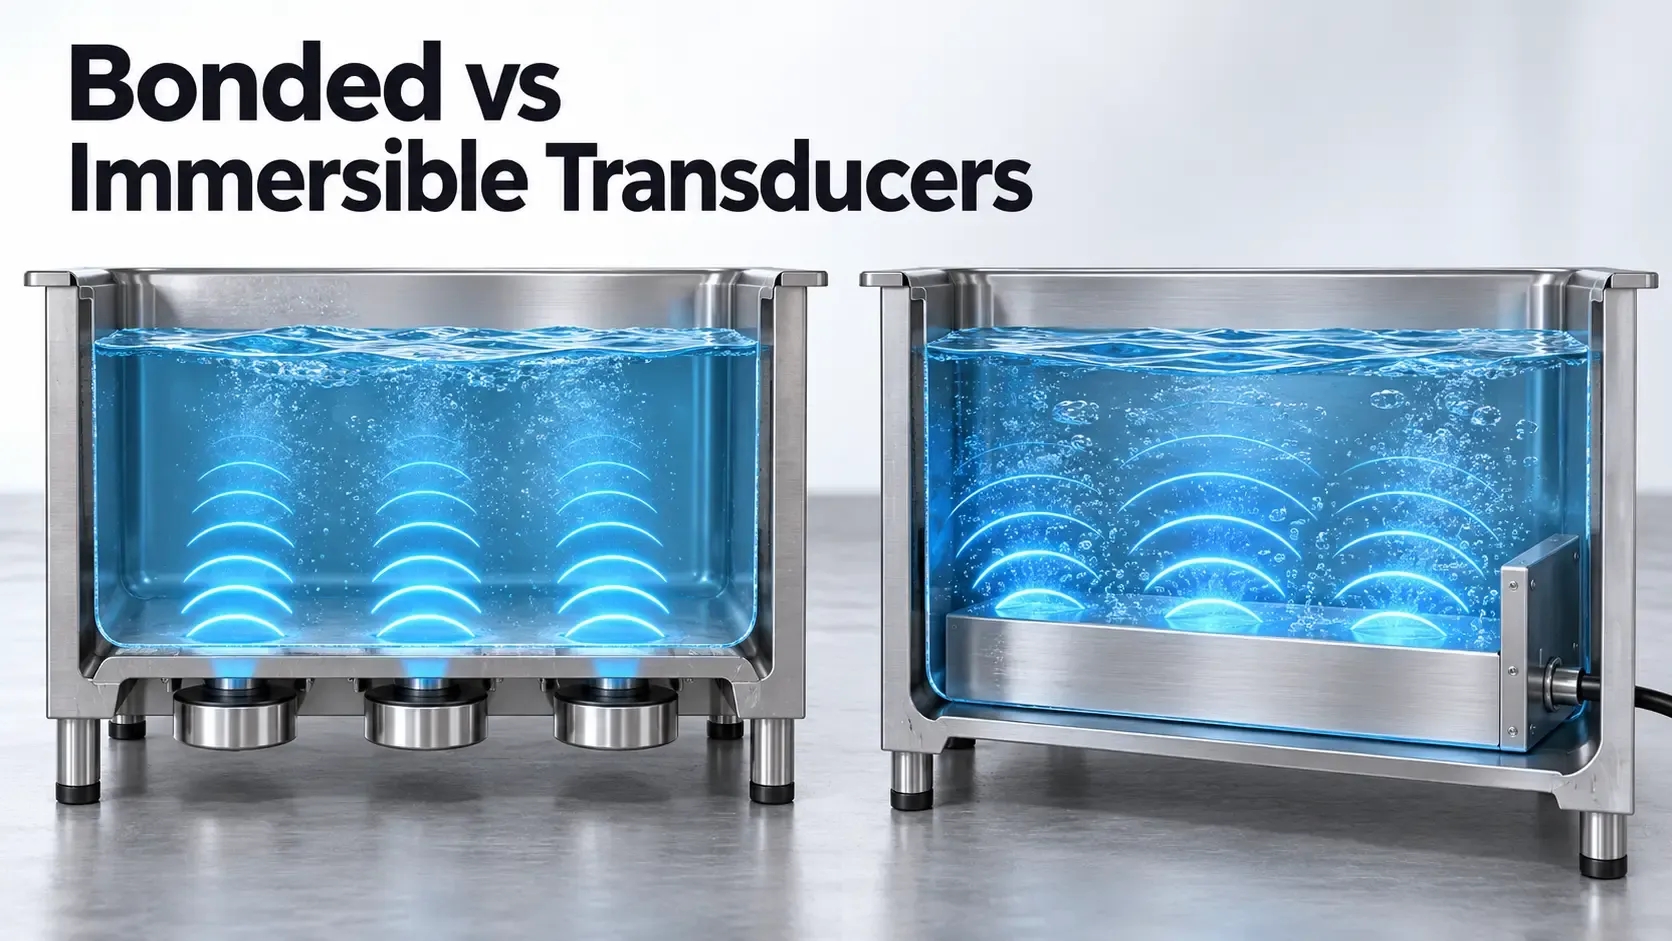
Sometimes an ultrasonic cleaner works, but cavitation is unevenly distributed.
This can cause some parts to clean well while others remain dirty.
Possible signs include:
- one side of the tank cleans better than the other
- foil damage appears only in certain areas
- the center of the basket cleans poorly
- parts near the bottom clean differently from parts near the top
- cleaning results change depending on part position
- repeated failures occur in the same tank zone
Possible causes include:
- incorrect liquid level
- overloaded basket
- poor part spacing
- parts shadowing or blocking ultrasonic energy
- missing degassing step
- poor basket or fixture design
- uneven equipment performance
- tank design limitations
Before assuming the machine is broken, reduce the load, space out the parts, and retest.
If results improve with fewer parts, the issue may be loading density, not machine failure.
7. Rule Out Process Problems Before Blaming the Machine
Many cleaning failures stem from process variables rather than hardware malfunction.
Before declaring the cleaner faulty, verify:
- cleaning chemistry compatibility
- detergent concentration
- bath age and contamination load
- solution temperature
- cleaning time
- part orientation
- basket design
- post-cleaning rinsing and drying
Related troubleshooting guides:
If the same machine cleaned well before and now performs poorly under the same controlled conditions, equipment condition should be investigated.
8. When Weak Cleaning May Indicate Equipment Problems
After ruling out setup, chemistry, and loading issues, persistent weak cleaning may indicate equipment wear or malfunction.
Potential equipment-related red flags include:
- cleaning performance has steadily declined over time
- foil test results are significantly weaker than previous reference tests
- a specific tank zone remains consistently inactive after load reduction
- the machine makes unusual sounds compared with normal operation
- heating works, but ultrasonic cleaning action appears weak
- timer works, but cleaning action is poor
- results do not improve after degassing, solution change, or load reduction
Possible causes may include:
- aging transducers
- generator issues
- poor electrical connection
- damaged tank structure
- incorrect power output
- long-term wear
Do not open or service internal electrical components unless qualified.
If equipment issues are suspected, contact the supplier with test records, foil photos, machine model, and operating details.
9. Safety Precautions: What Not to Do
When troubleshooting a weak ultrasonic cleaner, avoid unsafe or misleading checks.
Do not:
- put bare hands into an operating ultrasonic bath
- touch or press against the tank bottom during operation
- run the machine dry
- operate with incorrect liquid level
- use flammable solvents unless the system is specifically designed for that use
- open electrical enclosures or generator cabinets without qualification
- assume electronic sound equals effective cavitation
- assume one foil test proves full process validation
- keep increasing time, heat, or chemical strength without checking material compatibility
Safety and process control matter as much as cleaning performance.
Troubleshooting Guide
Observation | Possible Cause | What to Check |
|---|---|---|
Machine hums or buzzes but does not clean | Wrong chemistry, no degassing, weak cavitation | Check setup, degas the bath, perform foil test |
Foil test shows no marks or holes | Weak or absent ultrasonic activity | Verify liquid level, degassing, and machine condition |
Foil damage appears only in one zone | Uneven cavitation or dead zone | Check test position, load distribution, basket, and tank area |
Cleaning improves after running empty | Dissolved air was reducing cavitation | Add degassing routine before cleaning |
Cleaning improves with fewer parts | Basket overloading or acoustic shadowing | Reduce batch size and improve part spacing |
Cleaning degrades as the day progresses | Solution is saturated with oil, chips, or contamination | Check bath age, oil load, and filtration |
Heating works, but cleaning action is weak | Ultrasonic system may be weak | Conduct foil test and contact supplier for diagnostics |
Machine worked before but now performs poorly | Process change or equipment wear | Compare setup, test results, and historical performance |
What Information to Send Sonixmax for Diagnosis
If you are uncertain whether your ultrasonic cleaner is functioning correctly, gather the following details before contacting support:
Information | Why It Matters |
|---|---|
Machine model, tank size, and age | Helps understand equipment capability and condition |
Cleaning solution and concentration | Helps separate chemistry issues from equipment issues |
Liquid level | Affects cavitation performance |
Whether the bath was degassed | Helps diagnose weak early-cycle cavitation |
Temperature and cycle time | Helps evaluate operating setup |
Part material and contamination type | Helps separate process issues from machine issues |
Basket or fixture photos | Helps identify blocked cavitation or overloading |
Foil test photos | Helps compare cavitation activity |
Before-and-after part photos | Shows cleaning result pattern |
Whether performance changed over time | Helps identify equipment wear or process changes |
Clear operating details make troubleshooting much faster than saying only “the machine is not working.”
Need Help Checking Ultrasonic Cleaning Performance?
If your ultrasonic cleaner makes sound but does not clean well, send Sonixmax your machine information, cleaning solution, liquid level, degassing condition, basket setup, foil test photos, and part cleaning results.
Sonixmax can help evaluate whether the problem is related to process settings, cavitation distribution, loading, bath condition, cleaning chemistry, or equipment configuration.
The goal is not only to confirm that the machine runs. The goal is to make sure the cleaning process produces stable, repeatable results.